English
 中文简体
 русский
 Español
 عربى
Rated Voltage 3.6/6kV–26/35kV XLPE Insulated Power Cable: Design, Performance, Applications, and Manufacturing Excellence
Content
- 1 1. Product Overview
- 2 2. Why XLPE Insulation Is Important
- 3 3. Multilayer Cable Construction
- 4 4. Main Cable Types and Applications
- 5 5. Electrical and Thermal Performance
- 6 6. Quality and Safety Testing
- 7 7. Manufacturing Process and Technical Strength
- 8 8. Advantages Compared with Alternative Cable Solutions
- 9 9. Company Manufacturing Capability
- 10 10. Application Areas
- 11 11. Installation and Engineering Considerations
- 12 12. Cable Selection Checklist
- 13 13. Frequently Asked Questions
- 14 Product: Rated Voltage 3.6/6kV–26/35kV XLPE Insulated Power Cable
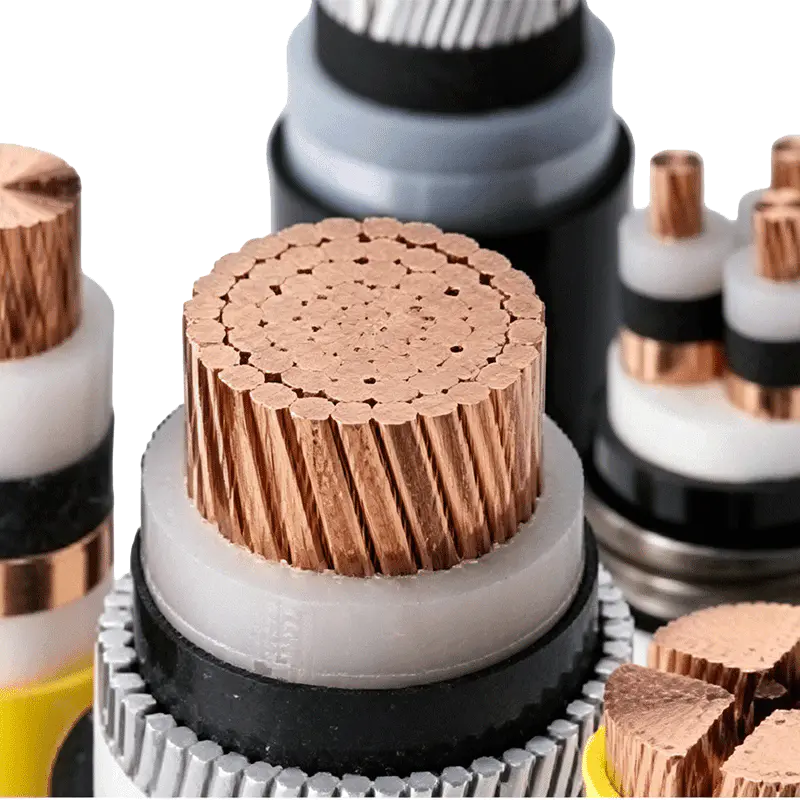
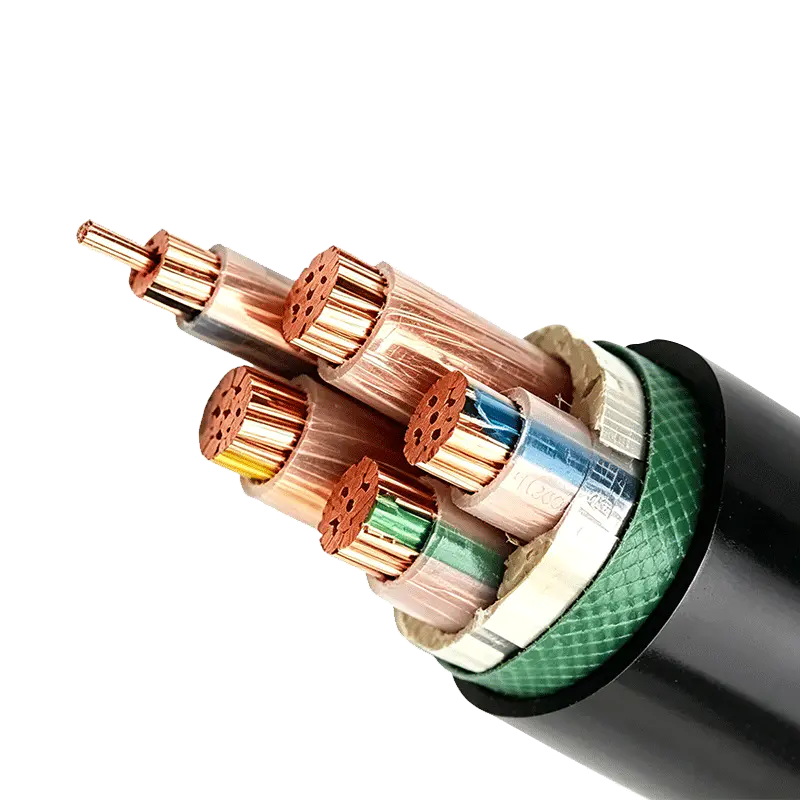
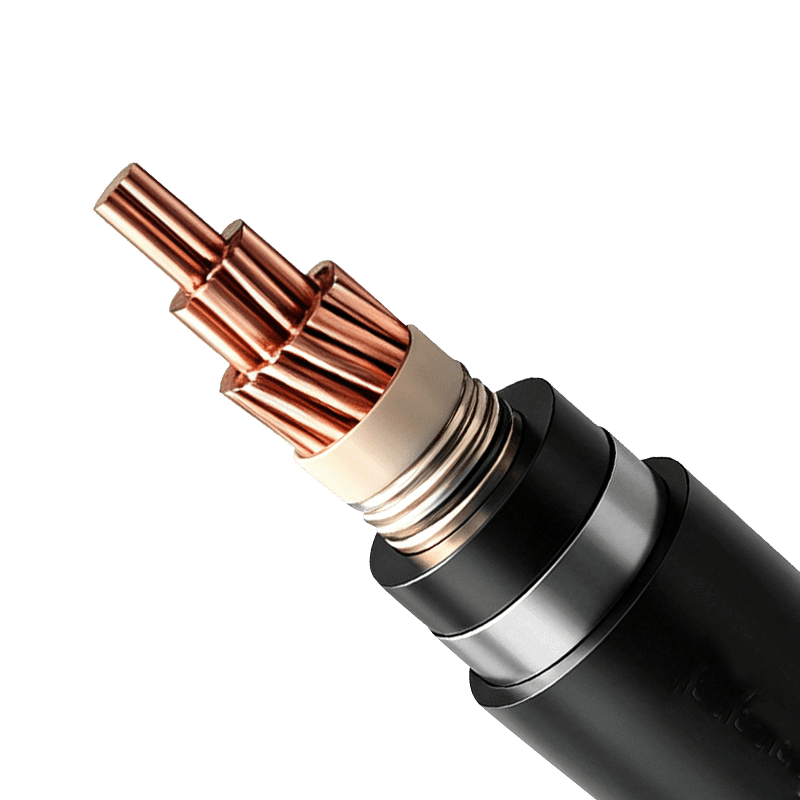
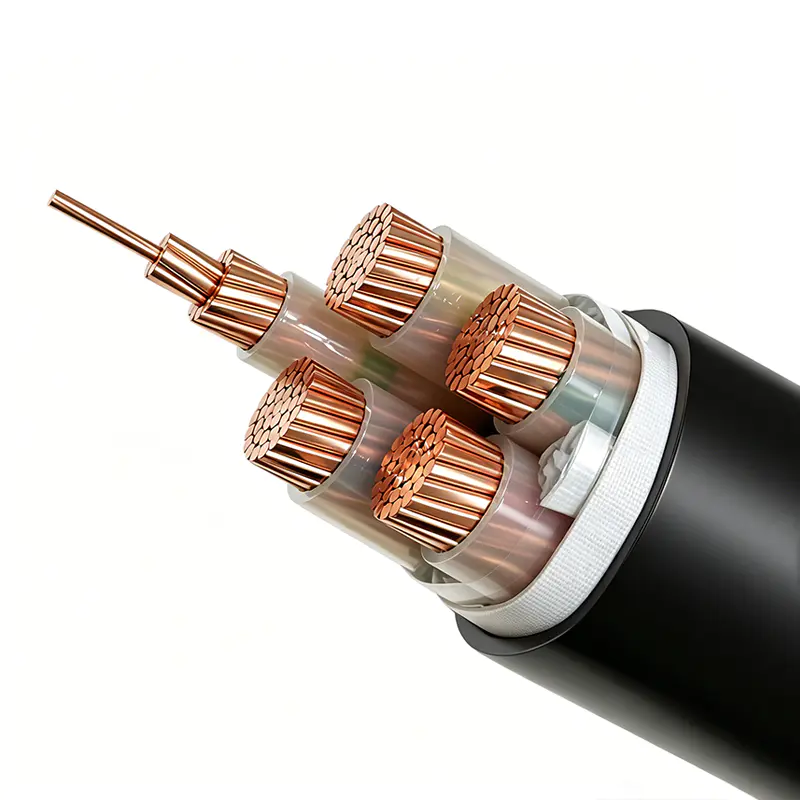
Reliable medium- and high-voltage power transmission depends on cable systems that can withstand electrical stress, thermal loading, mechanical forces, moisture, chemical exposure, and demanding installation conditions. The rated voltage 3.6/6kV–26/35kV XLPE insulated power cable is designed for these requirements. It combines a high-purity copper or aluminum conductor with cross-linked polyethylene insulation, semiconductive screens, a metallic screen, and a protective outer sheath. Depending on the installation environment, the cable may also include steel tape or steel wire armoring.
This cable family is intended for fixed power transmission and distribution installations. It can be used in urban distribution networks, industrial plants, infrastructure projects, substations, tunnels, cable trenches, and direct-buried systems. Its rated voltage range covers commonly required system classes, including 3.6/6kV, 6/10kV, 8.7/15kV, 12/20kV, 18/30kV, 21/35kV, and 26/35kV.
The product is manufactured by Wuxi Guanghuan Cable Co., Ltd., a Chinese cable manufacturer with extensive experience in power cables, electrical equipment wires, overhead conductors, railway cables, renewable-energy cables, and other specialized cable systems. The company combines large-scale production capacity, testing resources, technical personnel, process control, and certification systems to support consistent product quality.
Compared with many conventional thermoplastic-insulated cables, XLPE insulated power cable offers higher continuous operating temperature, improved insulation stability, better resistance to aging, and a more favorable current-carrying capability. Its multilayer construction also provides effective control of the electrical field and enhanced protection against mechanical and environmental damage.
Rated Voltage 3.6/6kV–26/35kV XLPE Insulated Power Cable
1. Product Overview
The 3.6/6kV–26/35kV XLPE insulated power cable is an extruded-insulation power cable designed for three-phase power transmission and distribution. The cable is suitable for systems in which electrical energy must be transferred safely over medium or long distances while maintaining insulation reliability under continuous operating conditions.
XLPE, or cross-linked polyethylene, is produced by transforming polyethylene molecules from a predominantly linear structure into a three-dimensional network structure. This cross-linking process changes the behavior of the material from thermoplastic to thermosetting. As a result, the insulation can maintain its mechanical and electrical properties at elevated temperatures without softening in the same way as ordinary thermoplastic polyethylene.
The cable is normally selected according to the system voltage, conductor material, conductor cross-sectional area, number of cores, installation method, short-circuit level, mechanical requirements, and environmental conditions. The available construction may be unarmored or armored, and the sheath may be made from PVC or PE according to the intended application.
The principal product advantages include:
• A rated voltage range suitable for medium- and high-voltage distribution systems.
• XLPE insulation with a maximum long-term conductor operating temperature of 90°C.
• A maximum conductor short-circuit temperature of 250°C for a short circuit lasting no more than five seconds.
• Extruded conductor and insulation screens that provide controlled electrical-field distribution.
• Copper tape or copper wire metallic screening for grounding and short-circuit current paths.
• PVC or PE outer sheathing for protection against moisture, abrasion, and environmental exposure.
• Optional steel tape armoring for resistance to certain external mechanical forces.
• Optional steel wire armoring when tensile strength and pulling resistance are required.
• Copper and aluminum conductor options for different project budgets, transmission requirements, and installation conditions.
• Compatibility with indoor, tunnel, trench, and direct-buried installation methods.
2. Why XLPE Insulation Is Important
Insulation is one of the most important parts of a medium- or high-voltage cable. It must prevent current from flowing between the conductor and the metallic screen while withstanding electrical stress over many years. It must also tolerate thermal cycling, installation forces, moisture, and occasional overload conditions.
Cross-linked polyethylene provides a combination of properties that is well suited to these requirements. Its molecular network gives it strong thermal stability, good mechanical strength, low dielectric losses, and high insulation resistance. These characteristics help the cable maintain stable performance when the conductor temperature rises during normal operation or short-duration overloads.
The 90°C maximum continuous conductor temperature allows the cable to carry more current than many cables using lower-temperature insulation, provided that the installation conditions and thermal calculations support the selected rating. A higher permissible operating temperature can also allow a project to use a smaller conductor for a defined load, although conductor selection must always be confirmed through a complete engineering calculation.
XLPE insulation also supports compact cable construction. Because the insulation offers high dielectric strength, the cable can achieve the required voltage performance without excessive insulation thickness. A compact construction can simplify transportation, handling, cable routing, and termination work.
Another benefit is resistance to aging. The cross-linked structure is less susceptible to deformation under heat and pressure than ordinary thermoplastic insulation. When the cable is correctly designed, manufactured, installed, and operated, this contributes to stable long-term service performance.
Compared with oil-filled cable systems, XLPE cables do not require an oil supply system, pressure monitoring, or oil leakage control. Compared with some older paper-insulated technologies, they are generally lighter, easier to handle, and less complicated to install. Compared with basic low-voltage cable designs, the screened multilayer construction is specifically engineered to control electric fields at medium and high voltage.
3. Multilayer Cable Construction
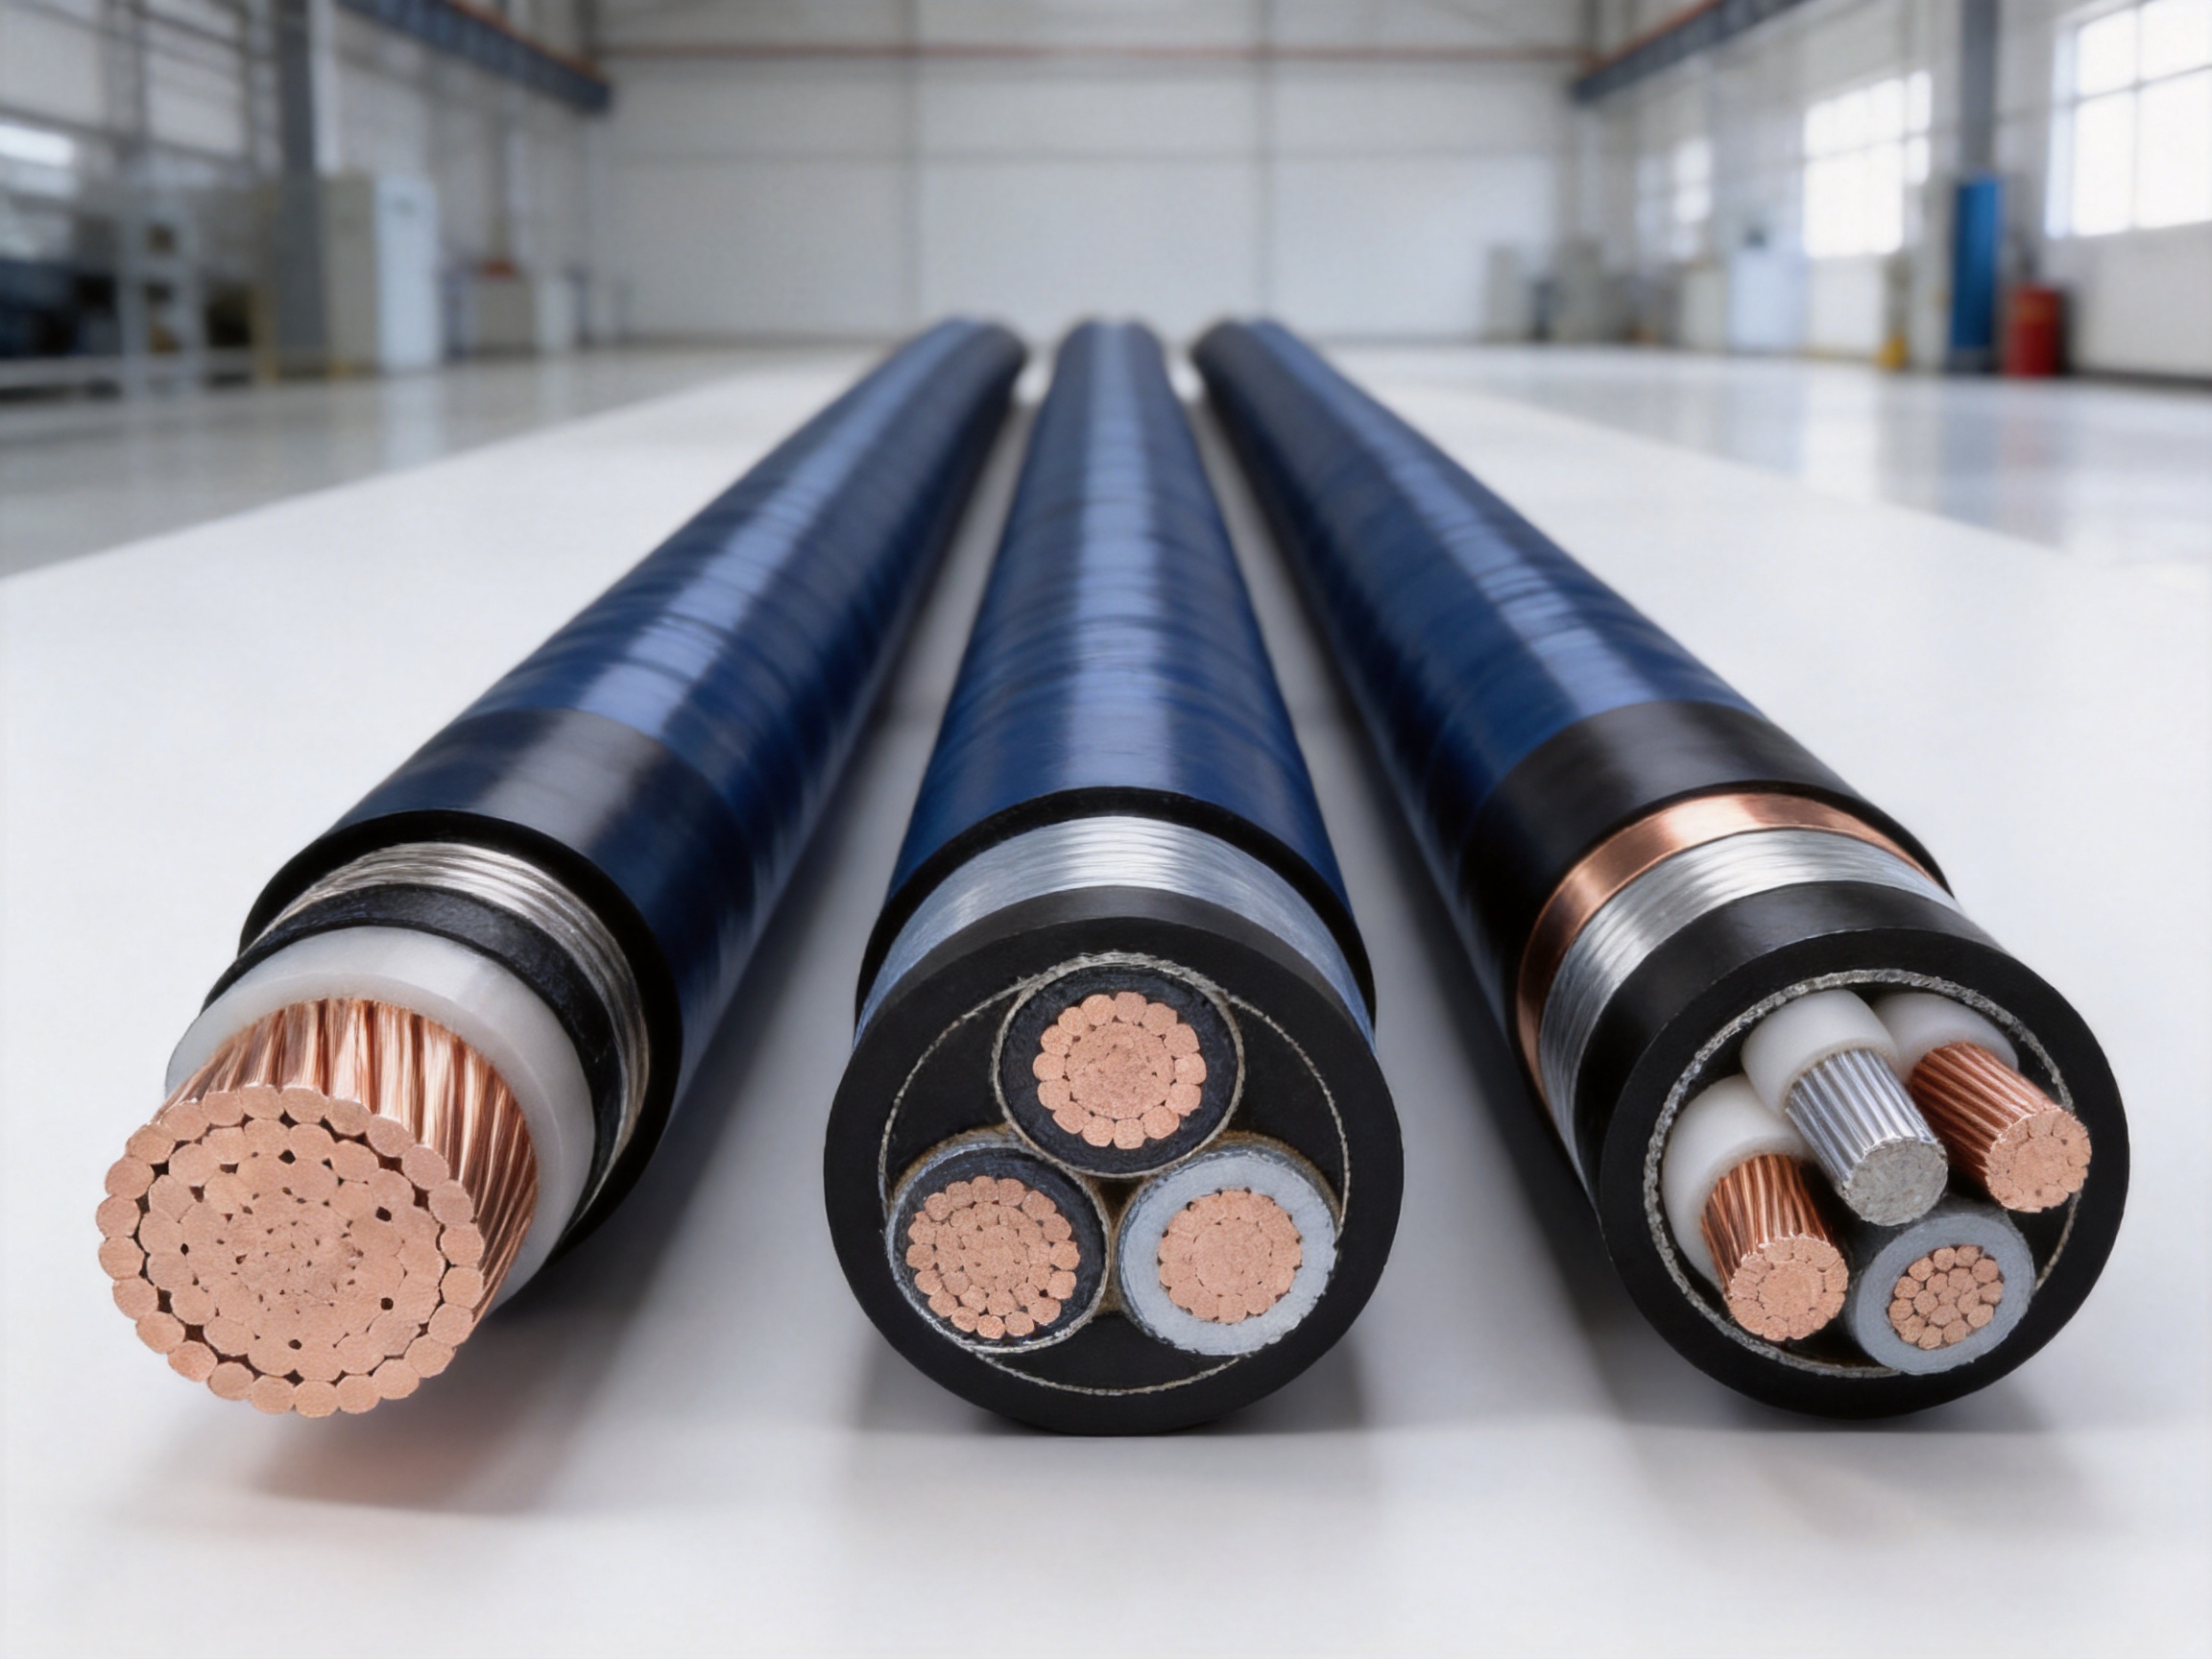
The cable is built as a coordinated system rather than as a conductor with a single insulation layer. Each layer performs a specific electrical, mechanical, or environmental function. The quality of the interfaces between layers is particularly important because defects, contamination, or poor adhesion can create local electrical stress and reduce service reliability.
3.1 Conductor
The conductor is manufactured from high-purity copper or aluminum. Copper provides high electrical conductivity, good flexibility, and strong short-circuit performance. Aluminum has a lower material density and can provide a lighter, more economical cable when the conductor size is selected appropriately.
The conductor cross-sectional area is selected according to the continuous load current, voltage drop, short-circuit current, installation conditions, and applicable standard. The available production range includes conductor sizes from 25mm² to 1000mm² for many single-core constructions and from 25mm² or 50mm² to 500mm² for many three-core constructions, depending on voltage class, conductor material, and cable type.
Conductor resistance is controlled in accordance with GB/T 3956. Lower conductor resistance helps reduce I²R losses, heat generation, and operating costs. Conductor quality also affects jointing, termination, bending behavior, and the cable’s ability to withstand short-circuit forces.
3.2 Conductor Screen
An extruded semiconductive conductor screen is applied over the conductor. Its purpose is to smooth the conductor surface and make the electrical field more uniform around the insulation. Without proper screening, irregularities at the conductor surface could create concentrated electrical stress.
The conductor screen also provides a controlled interface between the conductor and the XLPE insulation. This is especially important at medium and high voltage, where small imperfections can have a much greater effect than they would in a low-voltage cable.
3.3 XLPE Insulation
The XLPE insulation layer provides the primary dielectric barrier. Its thickness is determined by the rated voltage and the applicable manufacturing standard. The insulation must be uniform, clean, and free from voids, foreign particles, protrusions, and other defects.
During manufacturing, careful control of temperature, pressure, extrusion speed, material cleanliness, and cross-linking conditions is required. The objective is to produce a smooth insulation layer with stable thickness and consistent electrical properties throughout the cable length.
3.4 Insulation Screen
An extruded semiconductive insulation screen is applied over the XLPE insulation. It helps maintain a uniform electrical field and creates a controlled interface between the insulation and the metallic screen. A well-bonded screen reduces the possibility of localized stress concentrations.
The insulation screen is particularly significant during cable testing and operation. It must be continuous and properly integrated with the cable’s overall screening and grounding arrangement.
3.5 Metallic Screen
The metallic screen may consist of copper tape or copper wires. It provides a path for capacitive current, induced current, and earth-fault current. It also helps maintain the desired electrical-field boundary around the insulation.
For 21/35kV and 26/35kV cables, as well as some larger cross-sectional constructions, copper wire shielding may be used. In such cases, an “S” designation may be added to the cable model according to the applicable product coding practice. The metallic screen must be correctly connected and grounded during installation to ensure safe operation.
3.6 Filling and Binding Materials
For three-core cables, non-hygroscopic filling materials are used to fill the spaces between insulated cores. Non-woven binding tape may then be applied to hold the assembly together and maintain a stable circular form.
The use of non-hygroscopic materials helps limit moisture absorption within the cable assembly. Stable filling and binding also support a consistent outer diameter, improve handling, and provide a suitable base for the inner sheath or armor.
3.7 Inner Sheath and Armoring
An inner sheath may be included to separate the insulated cores from the armoring layer. Steel tape armor is suitable when the cable needs improved resistance to certain external compressive or longitudinal mechanical forces. Steel wire armor is used when greater tensile strength or pulling resistance is required.
Armoring selection should be based on the installation environment. A cable installed in a protected indoor cable tray may not require the same construction as a cable installed directly underground, in a well, or in an area exposed to mechanical impact.
3.8 Outer Sheath
The outer sheath is commonly made from PVC or PE. It protects the cable from moisture, abrasion, chemicals, sunlight, and general environmental exposure, depending on the selected material and formulation.
PVC sheaths are widely used because of their general-purpose mechanical and environmental performance. PE sheaths can be selected where particular moisture resistance, abrasion resistance, or other environmental properties are required. The final sheath selection should be matched to the project specification.
4. Main Cable Types and Applications
The cable family includes several common constructions. The model designation identifies the conductor material, insulation, sheath, and armor arrangement.
| Type | Construction | Typical Application |
|---|---|---|
| YJV | Copper conductor, XLPE insulation, PVC sheath | Indoor installation, tunnels, trenches, and direct burial where external mechanical forces are limited |
| YJLV | Aluminum conductor, XLPE insulation, PVC sheath | Similar applications to YJV where aluminum conductors are preferred |
| YJY | Copper conductor, XLPE insulation, PE sheath | Indoor, tunnel, trench, or direct-buried installations requiring a PE outer sheath |
| YJLY | Aluminum conductor, XLPE insulation, PE sheath | Power distribution installations using aluminum conductors and PE sheathing |
| YJV22 | Copper conductor, XLPE insulation, steel tape armor, PVC sheath | Installations requiring additional resistance to external mechanical forces |
| YJLV22 | Aluminum conductor, XLPE insulation, steel tape armor, PVC sheath | Armored distribution installations using aluminum conductors |
| YJV23 | Copper conductor, XLPE insulation, steel tape armor, PE sheath | Direct burial and other installations requiring steel tape armor and PE sheathing |
| YJLV23 | Aluminum conductor, XLPE insulation, steel tape armor, PE sheath | Armored aluminum-conductor installations |
| YJV32 | Copper conductor, XLPE insulation, fine steel wire armor, PVC sheath | Installations requiring mechanical protection and a defined pulling force capability |
| YJLV32 | Aluminum conductor, XLPE insulation, fine steel wire armor, PVC sheath | Mechanical-protection applications using aluminum conductors |
| YJV33 | Copper conductor, XLPE insulation, fine steel wire armor, PE sheath | Direct burial, wells, tunnels, and other demanding installations |
| YJLV33 | Aluminum conductor, XLPE insulation, fine steel wire armor, PE sheath | Demanding applications using aluminum conductors and PE sheathing |
Single-core cables are commonly used where high current capacity, installation flexibility, or special routing requirements make separate phase cables appropriate. Three-core cables can simplify installation in certain distribution systems by combining all phases into one cable assembly.
For single-core cables carrying alternating current, the installation method must be carefully considered. Magnetic effects can arise if ferromagnetic materials surround individual single-core cables. For this reason, single-core cable installation in a magnetic duct is generally not permissible unless the system is specifically designed to control these effects.
5. Electrical and Thermal Performance
The rated voltage U0/U is used to describe the cable’s electrical design. U0 is the rated power-frequency voltage between a conductor and earth or the metallic screen. U is the rated power-frequency voltage between conductors. Um is the maximum value of the highest system voltage that the equipment can withstand.
The cable range is intended for power-frequency systems from 3.6/6kV to 26/35kV. Selection must consider whether the system is effectively grounded, how long a single-phase earth fault may remain, and whether the application corresponds to the first or second cable class described in the product information.
The maximum long-term conductor operating temperature is 90°C. During a short circuit with a maximum duration of five seconds, the maximum conductor temperature is 250°C. These values are important when calculating continuous current ratings, emergency loading, and short-circuit withstand capability.
The short-circuit performance depends on conductor material, conductor area, initial temperature, final temperature, fault duration, and the installation system. The supplied technical data includes conductor short-circuit current values for common copper and aluminum conductor areas. Engineering calculations should use the exact cable design and actual fault duration rather than relying only on a general catalog value.
Current-carrying capacity is not a fixed value independent of the installation environment. It is affected by ambient air temperature, soil temperature, soil thermal resistivity, burial depth, cable spacing, the number of circuits, cable grouping, and whether the cable is installed in air or underground.
Reference conditions for the stated rating information include a maximum conductor temperature of 90°C, an air temperature of 40°C, a ground temperature of 25°C, soil thermal resistivity of 2.0K·m/W, a laying depth of 0.8m, and single-circuit operation. Single-core cables are considered installed in parallel with adjacent spacing equivalent to the cable diameter.
When actual conditions differ from these reference conditions, correction factors must be applied. For example, the air-temperature correction factor is 1.00 at 40°C, 0.94 at 45°C, and 0.90 at 50°C. For soil temperature, the factor is 1.00 at 25°C and decreases as soil temperature rises. Soil thermal resistivity also has a major effect: a value of 2.0K·m/W corresponds to a factor of 1.00, while a value of 3.5K·m/W produces a lower factor.
6. Quality and Safety Testing
Testing is essential for verifying that the cable is suitable for service. The product information specifies power-frequency AC voltage tests, four-hour AC voltage tests, impulse voltage tests, partial-discharge tests, conductor resistance measurements, and other electrical and dimensional checks.
6.1 Conductor Resistance Testing
Conductor DC resistance is measured at the specified reference temperature and compared with the requirements of GB/T 3956. This test confirms the electrical conductivity of the conductor and helps identify problems related to conductor material, strand quality, cross-sectional area, or manufacturing consistency.
6.2 Power-Frequency Withstand Testing
The five-minute power-frequency AC voltage test verifies the basic insulation withstand capability at the specified voltage class. A separate four-hour AC voltage test provides a longer-duration assessment of insulation integrity.
For the listed voltage classes, the five-minute test voltage rises from approximately 12.5kV for 3.6/6kV cable to approximately 91kV for 26/35kV cable, subject to the applicable standard and test arrangement. The four-hour test voltage similarly increases with the rated voltage.
6.3 Impulse Voltage Testing
Impulse testing evaluates the cable’s ability to withstand fast voltage surges such as those associated with lightning or switching events. The specified impulse test levels range from 60kV for 3.6/6kV cable to 250kV for 26/35kV cable.
Impulse performance is especially important in overhead-to-underground transitions, substations, industrial networks, and distribution systems exposed to switching operations. Correct system grounding, surge protection, termination design, and installation practice remain necessary in addition to the cable’s own impulse capability.
6.4 Partial-Discharge Testing
Partial discharge is a localized electrical discharge that does not completely bridge the insulation. It can be caused by voids, contaminants, protrusions, poor interfaces, or other defects. Over time, repeated partial discharge can cause insulation deterioration.
The product specification states that the maximum partial discharge at 1.73U0 shall not exceed 5pC. This requirement demonstrates the importance of clean materials, controlled extrusion, stable semiconductive screens, accurate temperature management, and high-quality testing equipment.
6.5 Routine and Process Control
Electrical tests are supported by process controls and physical inspections. These may include dimensional measurement, insulation thickness verification, eccentricity monitoring, sheath inspection, conductor examination, screen continuity checks, and review of material batches.
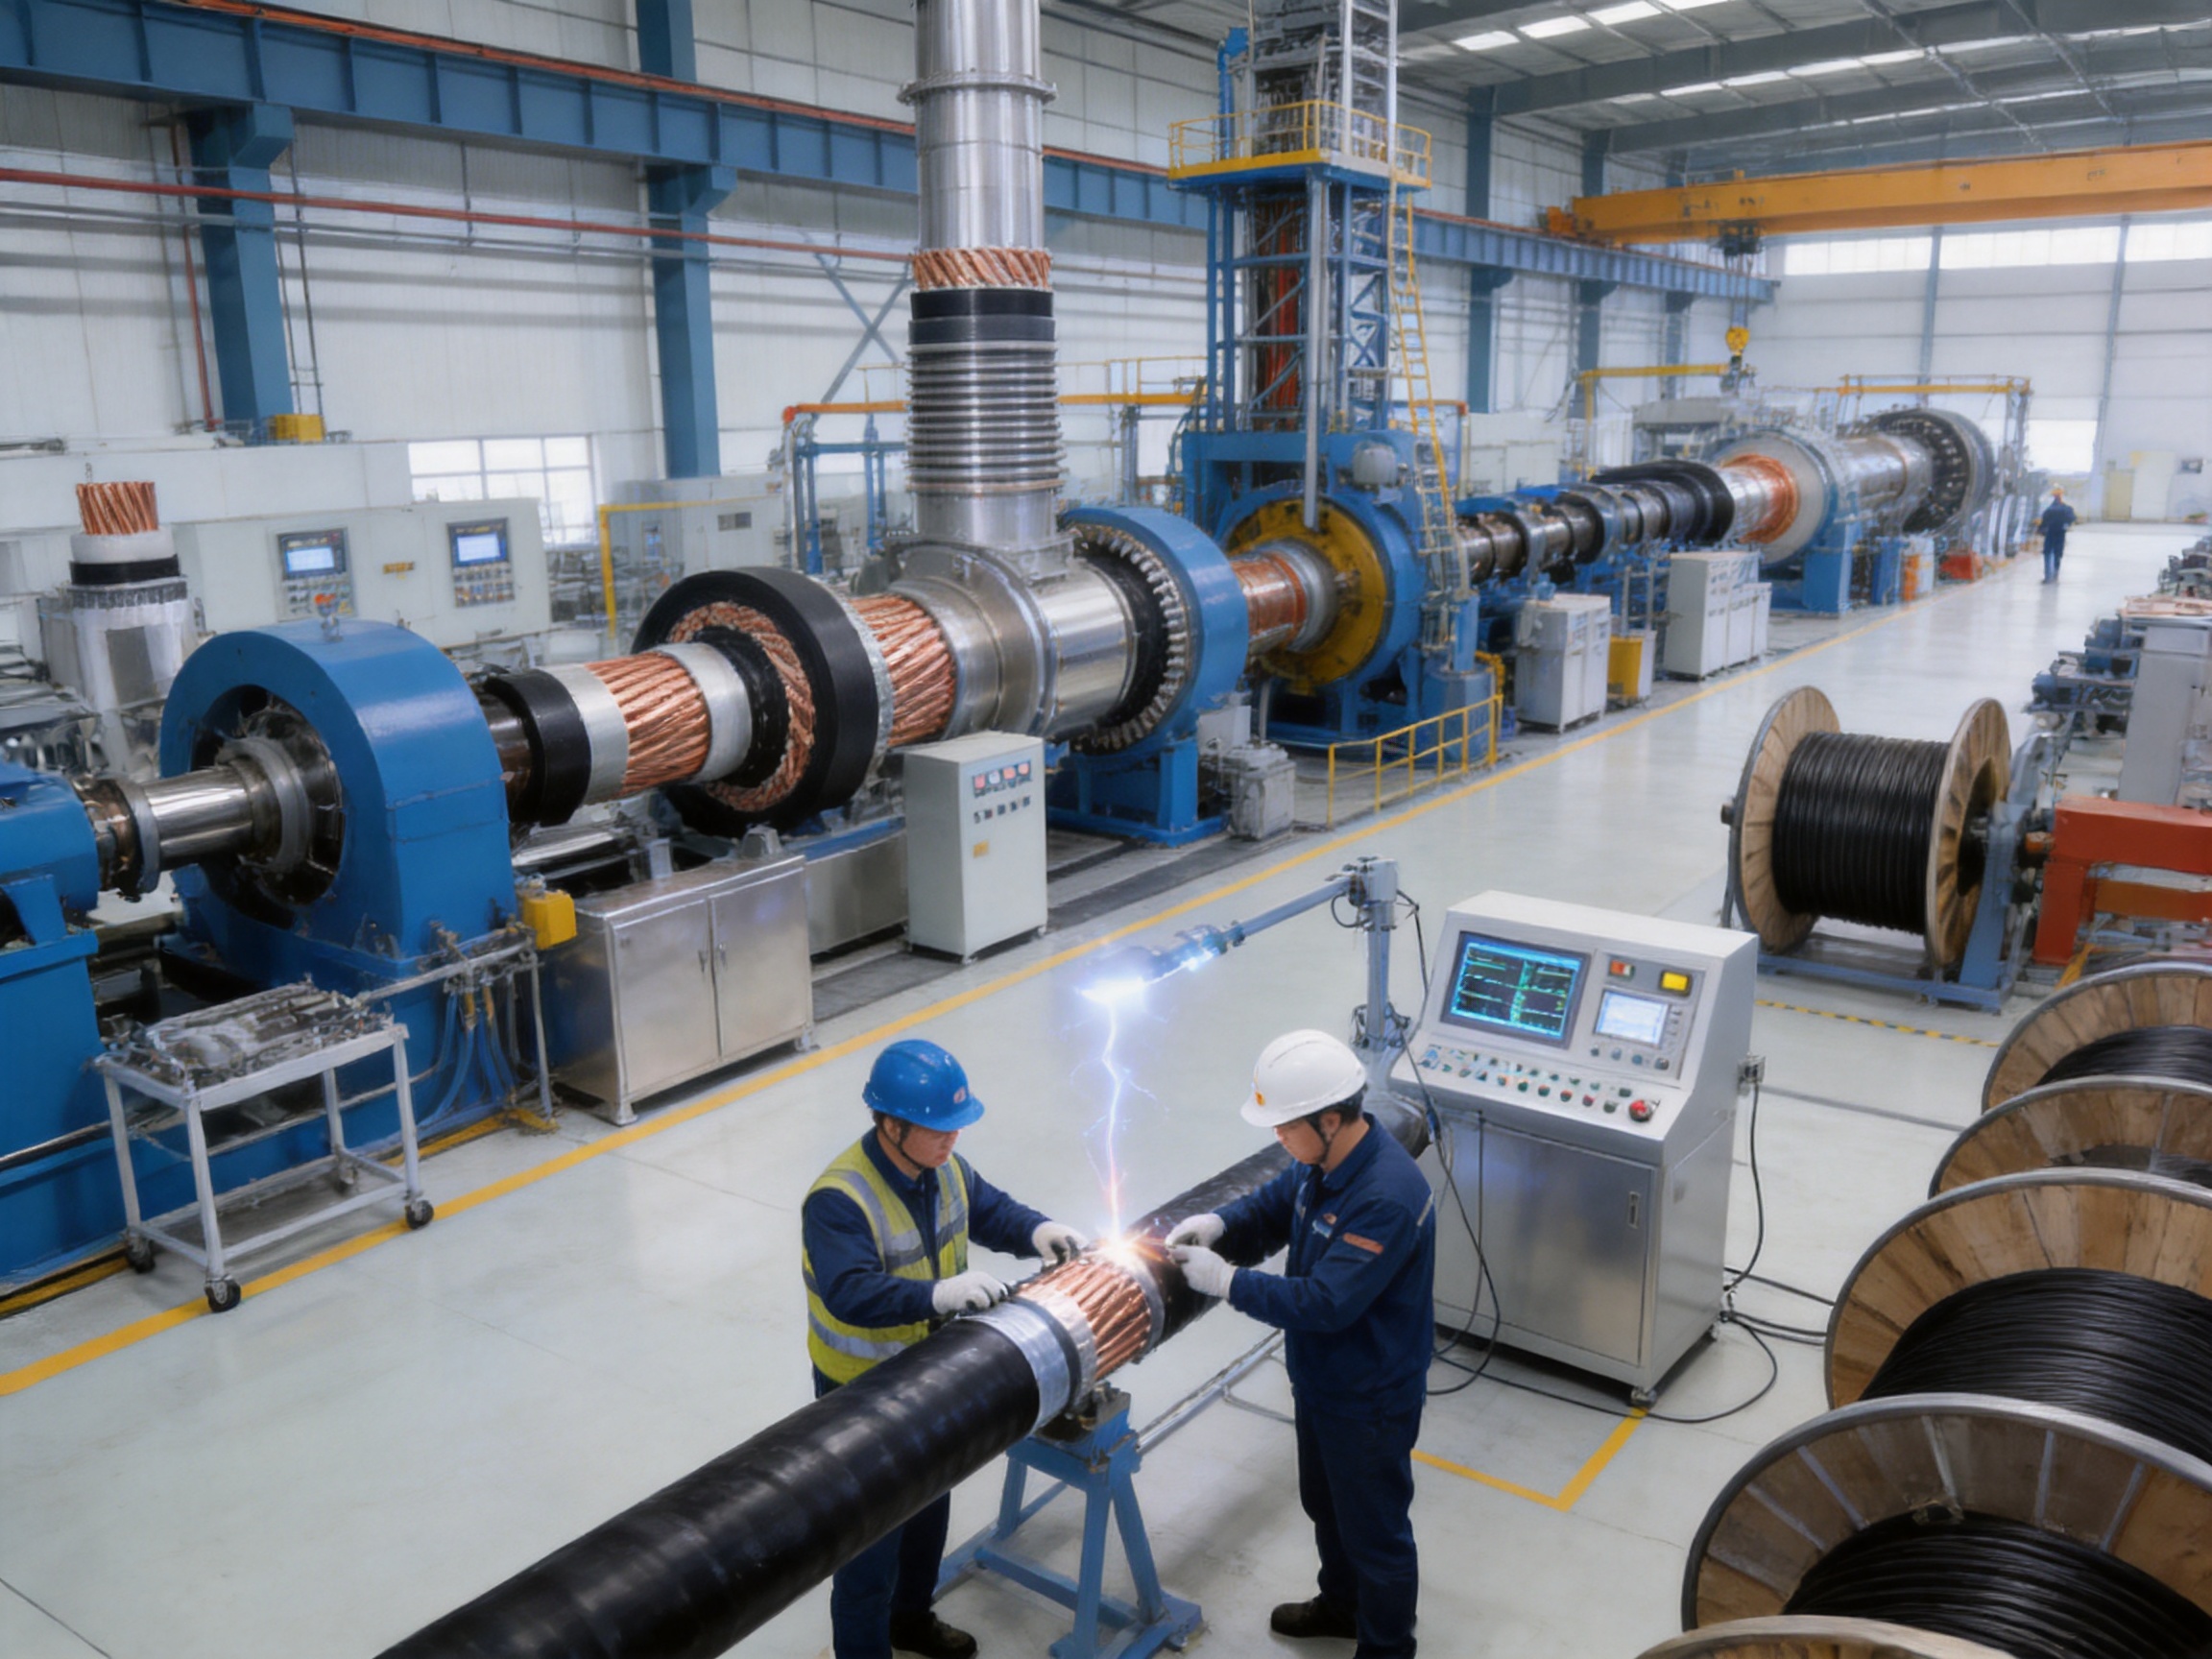
The manufacturer uses equipment such as online eccentricity monitoring systems, high-voltage series-resonance test systems, and partial-discharge detectors. These technologies help identify deviations during production and provide more reliable confirmation of the finished cable’s electrical performance.
7. Manufacturing Process and Technical Strength
Advanced cable manufacturing is not limited to the final test. Product reliability is built into every step, from raw-material selection to extrusion, cross-linking, screening, sheathing, inspection, and packaging.
7.1 Material Selection and Preparation
Conductors, semiconductive compounds, XLPE insulation compounds, metallic screens, fillers, tapes, armor materials, and sheath compounds must meet defined quality requirements. Material identification and batch control are important because variations in cleanliness, moisture, viscosity, or composition can affect cable performance.
XLPE compounds must be stored and handled in a controlled manner. Contamination or moisture can create defects in the insulation. A professional manufacturing system therefore emphasizes sealed material handling, controlled storage, production traceability, and inspection of incoming materials.
7.2 Conductor Production
Copper or aluminum wires are drawn, stranded, compacted, and prepared for insulation extrusion. Conductor geometry must be controlled to provide the required cross-sectional area, roundness, flexibility, and surface quality.
A smooth, uniform conductor surface supports better contact with the conductor screen and reduces the risk of localized electrical stress. Compaction can also help reduce the overall cable diameter while maintaining the required electrical performance.
7.3 Triple-Layer Co-Extrusion
For medium- and high-voltage XLPE cables, the conductor screen, XLPE insulation, and insulation screen are commonly applied through a coordinated extrusion process. This arrangement reduces the risk of contamination between layers and improves the consistency of the interfaces.
Process parameters such as extrusion pressure, melt temperature, line speed, material feed, and cooling conditions must be closely controlled. Online eccentricity monitoring helps confirm that the insulation remains centered around the conductor and that the screen layers are applied consistently.
7.4 Cross-Linking
After extrusion, the polyethylene insulation undergoes a cross-linking process. The process converts the material into a thermosetting structure with improved thermal and mechanical stability.
Uniform cross-linking is essential. If the process is incomplete or inconsistent, the insulation may not achieve the expected mechanical strength, thermal performance, or electrical reliability. The manufacturing line must therefore control temperature, pressure, residence time, and cooling conditions throughout the cross-linking cycle.
7.5 Screening, Assembly, and Sheathing
After the insulated core has passed inspection, the metallic screen is applied. Single-core cables may use copper tape or copper wire screening, while three-core cables are assembled with suitable filling and binding materials before the inner sheath or armor is applied.
Armor is applied according to the selected cable type. Steel tape armor provides a layered protective structure, while steel wire armor can provide increased tensile capability. The outer sheath is then extruded over the underlying construction and cooled under controlled conditions.
7.6 Inspection and Final Testing
The finished cable is inspected for dimensions, appearance, sheath integrity, marking, length, and electrical performance. Final testing confirms whether the product complies with the agreed standard, voltage class, construction, and customer specification.
This combination of online monitoring, process control, high-voltage testing, partial-discharge testing, and final inspection is a key advantage over manufacturing systems that rely only on limited end-of-line checks.
8. Advantages Compared with Alternative Cable Solutions
The 3.6/6kV–26/35kV XLPE cable offers several practical advantages when compared with other power cable technologies or less specialized constructions.
8.1 Higher Thermal Capability
With a 90°C maximum continuous conductor operating temperature, XLPE insulation supports higher permissible thermal loading than many lower-temperature insulation systems. This can improve power transmission capacity within an existing cable route, subject to installation and thermal calculations.
8.2 Improved Installation Convenience
The cable does not require an oil-pressure system or special fluid-management infrastructure. Its solid insulation and robust layered construction simplify storage, transport, installation, and maintenance compared with more complicated cable technologies.
8.3 Broad Installation Compatibility
Different combinations of conductor, sheath, and armor allow the cable to be adapted to indoor, tunnel, trench, direct-buried, well, and industrial installations. This flexibility can reduce the need to use entirely different product families for separate sections of a project.
8.4 Resistance to Environmental Conditions
XLPE insulation and appropriate sheath materials provide resistance to aging, moisture, chemical exposure, and mechanical wear. The exact level of protection depends on the selected sheath and armor, but the multilayer design is more adaptable than a simple unprotected insulated conductor.
8.5 Reduced Weight and Compact Construction
XLPE cable designs are generally lighter and more compact than many older oil-filled or paper-insulated alternatives. Lower weight can simplify cable pulling, support structure design, handling, and installation planning.
8.6 Electrical Stability
Semiconductive conductor and insulation screens help equalize the electrical field. Metallic screening provides a defined reference and fault-current path. These features are fundamental advantages over cable constructions that do not include appropriate medium-voltage field control.
8.7 Copper and Aluminum Options
The availability of both copper and aluminum conductors allows the cable to be selected according to the project’s electrical, mechanical, economic, and weight requirements. Copper may be preferred for higher conductivity and compactness, while aluminum can offer a lower-density and potentially more economical solution when the required cross-sectional area is acceptable.
9. Company Manufacturing Capability
Wuxi Guanghuan Cable Co., Ltd. was founded in 1998 and is headquartered in Guanlin Town, Yixing City, Jiangsu Province, a region recognized for its cable manufacturing industry. The company operates a production base covering more than 100,000 square meters, including more than 45,000 square meters of building area.
The company operates more than 70 production and testing lines and employs more than 140 people, including more than 30 technical professionals. Its reported annual sales revenue is approximately RMB 2 billion, with annual output value exceeding RMB 3 billion. These resources support production across power cables, electrical equipment wires and cables, bare conductors, overhead insulated cables, railway and urban rail transit cables, energy-storage cables, photovoltaic cables, wind-power cables, and other specialized products.
Its product portfolio includes more than 100 categories and over 30,000 specifications under the registered Liguang brand. This breadth of production experience is valuable because it exposes the manufacturing organization to different conductor sizes, insulation systems, voltage classes, sheath materials, screening arrangements, and application requirements.
The company has obtained ISO 9001 quality-management, ISO 14001 environmental-management, ISO 45001 occupational-health-and-safety, and ISO 50001 energy-management certifications. It has also obtained certifications and management-system recognitions related to intellectual property, green management, social responsibility, and after-sales service.
Product-related qualifications include CCC, TÜV, product carbon-footprint, and energy-saving and environmentally friendly product certifications for applicable products. The company has also passed qualification and capability verification for power cables and conductors conducted by the State Grid Corporation of China.
These credentials do not replace project-specific technical evaluation, but they demonstrate the presence of structured management systems, controlled manufacturing procedures, documented inspection practices, and experience with demanding power-sector requirements.
10. Application Areas
10.1 Urban Distribution Networks
Urban distribution systems require reliable underground cables that can be installed in trenches, ducts, tunnels, and direct-buried routes. XLPE cables are well suited to these applications because they offer compact construction, high insulation performance, and multiple sheath and armor options.
10.2 Industrial Facilities
Industrial plants often contain motors, transformers, switchgear, process equipment, and large electrical loads. The cable can be used for fixed connections between substations, distribution panels, transformers, and major production areas.
Industrial applications may expose cables to chemicals, heat, vibration, mechanical impact, or complex routing. The choice of PE or PVC sheath, steel tape armor, or steel wire armor should therefore be based on the site survey and project specification.
10.3 Infrastructure Projects
Large infrastructure projects such as transport facilities, water-treatment plants, public buildings, commercial complexes, and utility installations require dependable medium-voltage power distribution. The cable’s range of voltage classes and construction options supports different project scales.
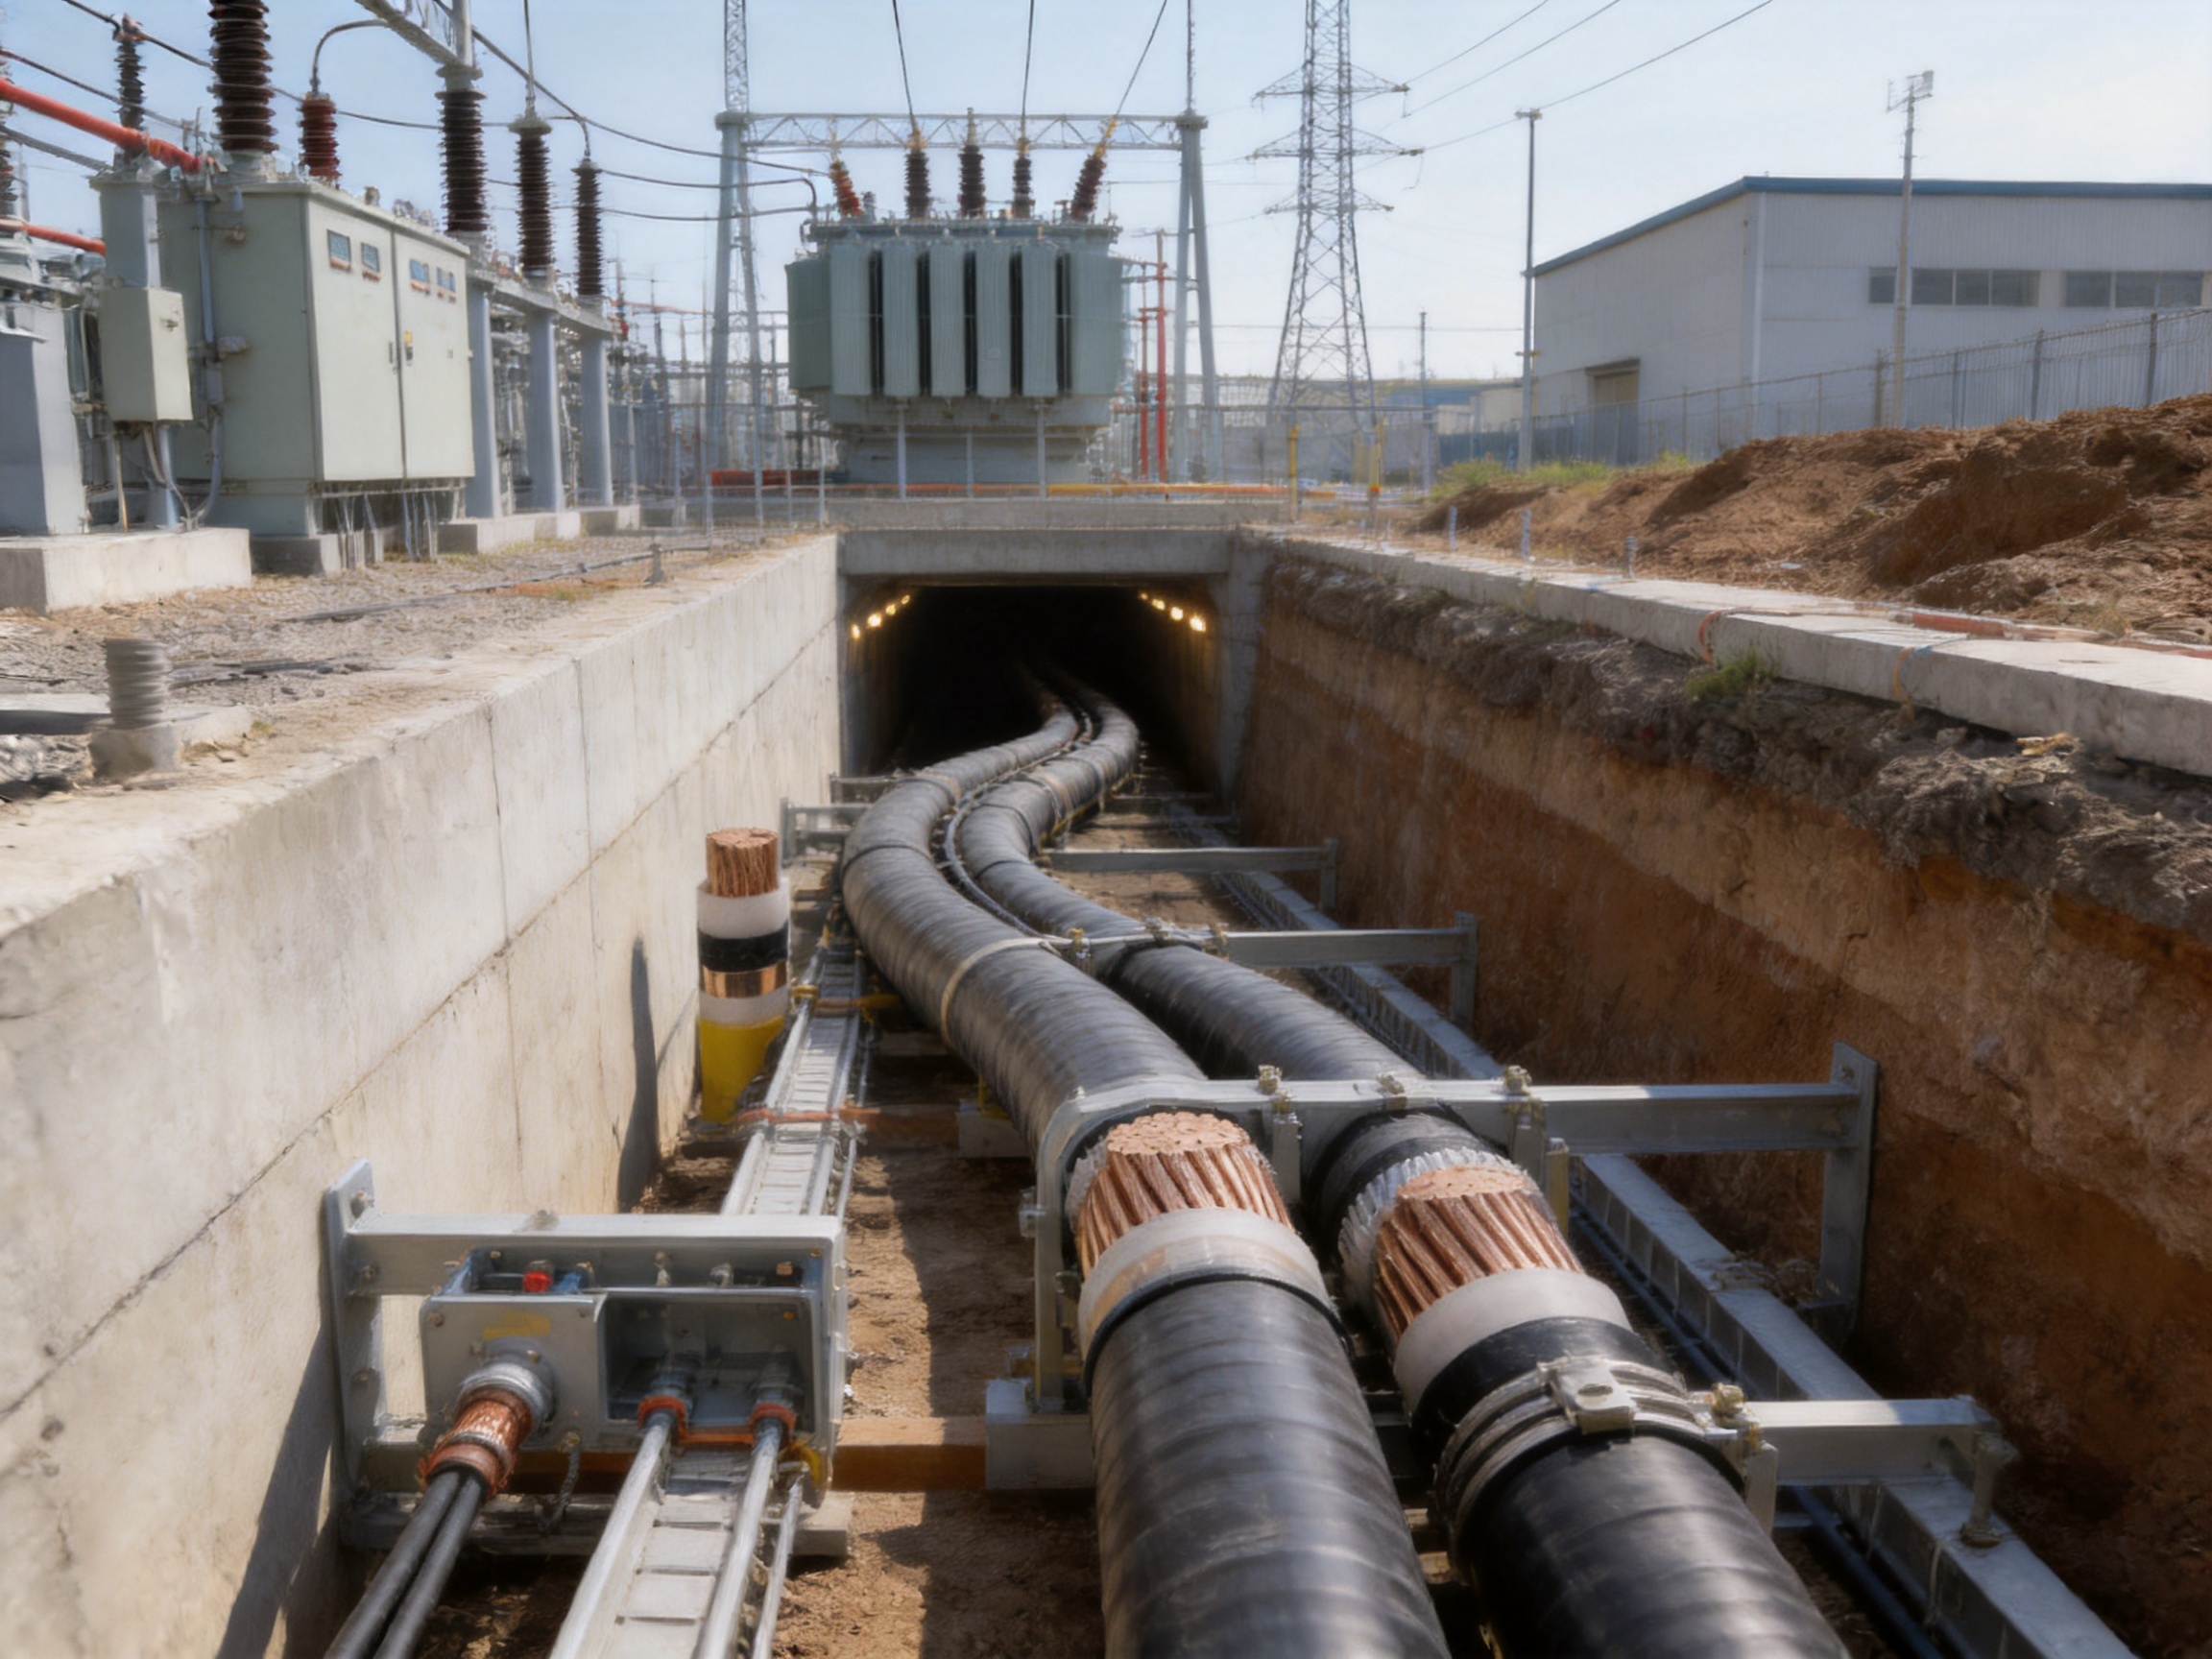
10.4 Tunnels and Cable Trenches
Tunnels and cable trenches require cables that can be routed through confined spaces and supported over long distances. The selected cable must be compatible with the bending radius, support spacing, ventilation conditions, fire-safety requirements, and mechanical exposure of the route.
10.5 Direct-Buried Systems
Direct burial can reduce construction cost and preserve space, but it exposes the cable to soil moisture, thermal resistance, ground movement, and possible mechanical damage. An armored construction and suitable outer sheath may be necessary. Cable spacing and soil thermal resistivity must be included in the current-rating calculation.
11. Installation and Engineering Considerations
The ambient temperature during installation should not be lower than 0°C. If the cable has been stored in cold conditions, it should be brought to a suitable temperature before bending and installation. Excessive cold can make sheath materials less flexible and increase the risk of damage during handling.
The minimum bending radius is generally not less than 15 times the cable outer diameter for three-core cable and not less than 20 times the cable outer diameter for single-core cable. The actual project specification may require a larger radius, particularly during pulling, jointing, termination, or installation around bends.
Pulling tension must be controlled. The permissible pulling force depends on conductor material, conductor cross-sectional area, armor construction, pulling method, cable length, route geometry, and the use of pulling eyes or other accessories. The cable should not be dragged over sharp edges or exposed to uncontrolled torsion.
Metallic screens must be bonded and grounded according to the system design. Single-core cable circuits may require special bonding arrangements to control circulating currents and induced voltages. The bonding method should be confirmed by a qualified electrical engineer.
Terminations and joints are part of the cable system and should be selected for the exact voltage class, conductor material, screen design, insulation diameter, and installation environment. A high-quality cable cannot compensate for an improperly installed termination or joint.
After installation, the cable route should be documented. Records should include cable type, length, drum number, phase identification, installation date, joint locations, termination locations, test results, and grounding configuration. This information simplifies future inspection and maintenance.
12. Cable Selection Checklist
Before ordering, users should provide the system rated voltage and maximum system voltage, number of cores, conductor material, conductor cross-sectional area, installation method, cable route length, short-circuit current, fault duration, ambient temperature, soil thermal resistivity, burial depth, and required sheath or armor.
The selection should also address whether the cable will be exposed to water, chemicals, ultraviolet radiation, rodents, impact, vibration, fire risk, or unusual pulling forces. Where the project includes parallel cables, the spacing and number of circuits must be provided for current-rating calculations.
For 21/35kV and 26/35kV systems, the metallic screen arrangement deserves particular attention. Copper wire screening may be required for higher voltage classes or larger conductor sizes. The screen area must be adequate for the expected fault-current duty and compatible with the grounding system.
Customers should confirm which standard applies to the project. The product is manufactured in accordance with GB/T 12706, including the sections covering cables rated from 6kV to 30kV and cables rated at 35kV. Production may also be arranged according to IEC, British, German, or American standards when required by the user and agreed in the technical specification.
13. Frequently Asked Questions
Q1: What voltage range does this cable cover?
The product covers power-frequency rated voltages from 3.6/6kV to 26/35kV. Common voltage classes include 3.6/6kV, 6/10kV, 8.7/15kV, 12/20kV, 18/30kV, 21/35kV, and 26/35kV.
Q2: What is the maximum continuous operating temperature?
The maximum permissible long-term conductor operating temperature is 90°C, provided that the cable is installed and operated in accordance with the applicable design conditions.
Q3: What temperature can the conductor reach during a short circuit?
During a short circuit lasting no more than five seconds, the maximum conductor temperature should not exceed 250°C.
Q4: Can the cable be used underground?
Yes. Depending on the construction, the cable can be installed directly underground, in cable trenches, ducts, tunnels, wells, or other fixed-installation environments. Armoring and sheath selection should match the expected mechanical and environmental
Product: Rated Voltage 3.6/6kV–26/35kV XLPE Insulated Power Cable
-
Rated Voltage 3.6/6kV–26/35kV XLPE Insulated Power Cable
-
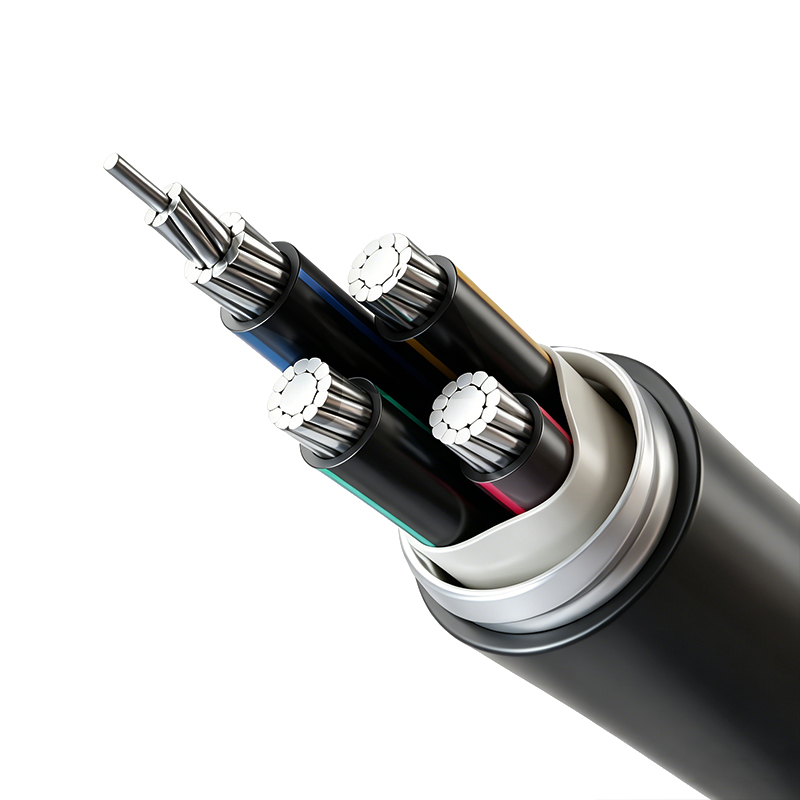
Aluminum Alloy Conductor Plastic Insulated Power Cable (Rated Voltage up to 26/35kV)
-
Rated Voltage 0.6/1kV XLPE Insulated Power Cable
-
Power Cable for Subway and Urban Rail Transit (Rated Voltage 35kV)
-
Rated Voltage 1.8/3kV XLPE Insulated Power Cable
Copyright © Wuxi Guanghuan Cable Co., Ltd. All Rights Reserved. Power Cables Manufacturer Electrical Wire And Cable Factory